Walk down any snack aisle and the product that catches your eye is rarely the best-tasting one. It’s the one that looks best in the package. A snack packaging pouch does more than hold food — it keeps the crunch crisp, blocks the light that turns oil rancid, and carries more visual real estate per dollar of packaging than almost any other format. And it does all of that in a package that weighs a fraction of what a jar or box weighs.
By the end of this guide, you’ll be able to specify a pouch that protects your product, clears food-contact compliance, looks premium on the shelf, and survives the sourcing process without surprise delays. We’ll cover materials and film structures, printing and color management, dieline design, sustainability claims that actually hold up, and the exact questions to ask a supplier before you commit.
Key Takeaways
- Define your barrier needs first — oxygen, moisture, and light requirements dictate film structure before any artwork is touched.
- Build artwork on the dieline, not flat. A pouch is a 3D object and text placed near seals or gussets will distort.
- Choose the print method by run length. Gravure, flexo, and digital each win at different volumes.
- Demand compliance documentation — migration reports, ink compliance, and food-contact certifications — before ordering, not after.
- Read MOQ and lead time alongside per-unit cost. They determine whether your first run is viable.
Why Your Snack Packaging Pouch Is the First Salesperson Your Product Has
Your packaging is on the shelf before you are. A shopper decides whether to pick up your product in roughly the time it takes to blink twice, and that decision is made almost entirely on what the package communicates. If the graphics are muddy, the type is too small to read from arm’s length, or the pouch looks cheap, none of the quality inside gets a chance to compete.
There’s also a functional argument. Flexible packaging keeps food fresher than rigid alternatives for many snack categories because it can be engineered with a precise barrier tailored to the product. The film can be tuned to let a breathable snack like fresh bread lose moisture while sealing out oxygen for a product prone to rancidity. That specificity is what custom snack packaging delivers — a package built around the actual chemistry of what you’re selling.
Across food categories, flexible formats have grown faster than rigid containers as brands chase lower shipping weight and stronger shelf presence. Industry research consistently points to that direction, and the practical reason is simple: less material per unit, less weight per pallet, and more billboard for the brand.

What Is a Snack Packaging Pouch? The Basics Before You Order
A snack packaging pouch is a flexible, sealed container made from laminated or co-extruded film layers, engineered to portion, protect, and merchandise snacks. It’s not “a bag” in the loose sense — it’s a precision package where each layer of film performs a specific job. The outer layer carries the print and resists scuffing. The middle layers block oxygen, moisture, and light. The inner seal layer keeps the product safe from the ink and adhesive and welds shut at high speed.
Why pouches beat rigid and carton options for most snack categories
Pouches win on three fronts weight, material, and presentation. A pouched product can weigh up to 80% less than the same volume in a glass jar, which compounds into real savings on freight and warehousing. Because a pouch uses less material per unit than a rigid container, the sustainability math often favors flexible packaging too, provided the film is chosen well.
But the biggest advantage is merchandising. A two-panel pouch gives you the entire face of a bag for graphics, while a carton is constrained by its rectangular shape and a jar is largely invisible from the front. For a snack that lives or dies on impulse, that extra print surface matters.
| Dimension | Flexible Pouch | Rigid Container | Carton / Box |
|---|---|---|---|
| Weight per unit | Lowest | Highest | Moderate |
| Protection level | Engineered to spec | High, but uniform | Moderate, lower barrier |
| Merchandising surface | Large front and back panels | Limited to label | Four faces |
| Material per unit | Least | Most | Moderate |
The Main Types of Snack Packaging Pouches (With a Comparison Table)
Pillow pouch / pillow bag
This is the bag you picture for single-serve chips and loose candy. It’s sealed on three sides, pillow-shaped in the middle, and it’s the most cost-efficient format per unit because it uses the least film. The trade-off is shelf presence — a pillow bag has to lean, so its front panel is only fully readable at one angle.
Stand-up pouch
The stand up pouch for snacks is the workhorse format for granola, trail mix, dried fruit, and protein snacks. A gusset at the base lets the bag stand on its own, giving you a full flat front panel for branding. Add a resealable zipper and you get a package that keeps product fresh after the first opening — a real value driver for products eaten over multiple sittings.

Flat-bottom / quad-seal pouch
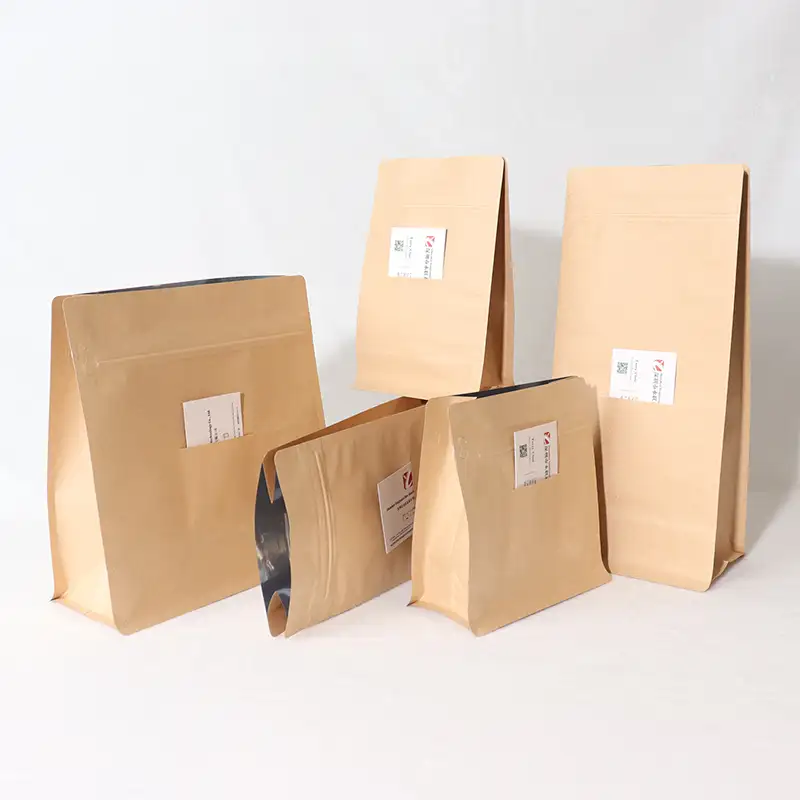
This is the premium option. A flat bottom gives the pouch a stable base and a shelf posture closer to a box, and the four seal edges create a larger billboard for graphics. It looks substantial and reads as “premium” automatically. The cost is more material per unit and slightly more complex production.
Sachet / single-serve stick pack
For portioned snacks — a single serving of coffee, protein powder, or a one-bite treat — the stick pack or sachet delivers exact portioning with minimal material. These are particularly useful for multipack programs and for products sold in retail singles.
Spouted pouch and specialty formats
Spouted pouches matter only for runny or paste-like products, which is a narrow slice of the snack category. We mention them for completeness, but for most snack brands, a spout isn’t on the table. Focus instead on the four formats above.
| Pouch Type | Best For | Brand Impact | Material Efficiency | Typical Use Case |
|---|---|---|---|---|
| Pillow pouch | Single-serve items | Moderate | Highest | Chips, candy, small cookies |
| Stand-up pouch | Multi-serve snacks | High | High | Granola, trail mix, dried fruit |
| Flat-bottom | Premium SKUs | Highest | Moderate | Gourmet snacks, gift sets |
| Stick pack | Portion control | Low | Highest | Single-serve powders, bites |
Materials and Film Structure — Protecting Flavor, Crunch, and Shelf Life
How a multi-layer lamination actually works
A snack pouch isn’t one sheet of plastic — it’s several films bonded together, each with a job. Think about it as a three-part team. The outer layer is the print surface; it needs to accept ink well, resist scuffing, and give the pouch structural stiffness. The middle layers are the barrier team; they stop oxygen, moisture, and light from reaching the food. The inner seal layer is what welds the pouch shut at high speed on the filling line, and it’s what touches your product.
Co-extrusion pushes several resins through one die to make a single film with layered properties. Lamination instead bonds two or more pre-made films together with adhesive. Both approaches are valid; the right one depends on your barrier spec, your printing method, and your budget.
Barrier properties that matter for snacks
Each snack fails differently. Potato chips go stale from oxygen and humidity. Nuts go rancid from oxygen plus light. Cookies go soft from moisture. A film structure is selected backward from the failure mode you’re trying to stop.
| Barrier Function | What It Protects Against | Snack Problem Solved |
|---|---|---|
| Oxygen barrier | Oxidation & rancidity | Nuts go stale, oils turn |
| Moisture barrier | Humidity transfer | Cookies soften, chips lose crunch |
| Light / UV barrier | Photodegradation | Dried fruit and nuts discolor |
| Aroma retention | Volatile loss | Flavored snacks lose their punch |
| Grease / oil resistance | Oil migration | Fried snacks stain or leak |
Common film types and thickness
The main players are familiar acronyms. BOPP gives high clarity, print quality, and stiffness. PET (polyester) offers strength and moderate barrier. Nylon (polyamide) adds puncture resistance and flex-crack resistance for sharper contents. Aluminum foil provides the best oxygen and light barrier of all, but it’s opaque, deadens the crunch of the package, and is harder to recycle. The sealant layer is typically PE (polyethylene), which welds reliably at low temperatures.
As spec guidance, total film thickness for a snack pouch commonly runs from around 60 to 130 microns. Stand-up pouches with a zipper usually sit on the thicker end because the structure needs body to stand; a single-serve pillow bag can go much thinner. A good film spec for fried snacks might be a BOPP/foil/PE laminate around 100 microns, while a dry granola stand-up pouch might run a PET/PE structure closer to 80.

Resealability and easy-open features
Zippers, tear notches, and laser scoring all solve different problems. A zipper adds value for any multi-serve product — granola, trail mix, dried fruit — because it keeps the product fresh after the first open. A tear notch makes a pouch easy to open without scissors, which matters for on-the-go snacking. Laser scoring creates a controlled tear line that gives a cleaner opening than a plain notch. Match the feature to how your consumer actually uses the product.
Printing Methods and Color Management — Getting the Brand Right the First Time
Rotogravure, flexography, and digital printing — the honest differences
Rotogravure engraves the image into a cylinder and transfers ink from the engraved cells. It’s the highest-quality option for photographic detail and fine gradients, and it’s the most economical at very high volumes because the plate cost is spread across a large run. But you’re paying for cylinder engraving up front, which is why it doesn’t make sense for small batches.
Flexography uses flexible rubber or polymer plates and works in rotary presses. It’s a strong all-rounder, especially for bold solid colors and line art, and it’s cost-effective at medium runs. Digital printing puts the image straight from a file onto the film — no plates at all — which makes it ideal for short runs, frequent design refreshes, and regional variations without re-plating costs.
| Method | Typical Run Size | Finish Quality | Design Complexity | Turnaround |
|---|---|---|---|---|
| Rotogravure | High volume | Best (photos & gradients) | Highest | Longer (cylinder prep) |
| Flexography | Medium volume | Very good (bold color) | Moderate | Moderate |
| Digital | Short runs | Good, no plates | High flexibility | Fastest |
Color management and proofing
Packaging is printed in CMYK process color plus spot colors for brand-critical tones. If your brand has a signature orange or a specific green, it’s almost certainly a pantone spot color, and it needs to be locked in, not approximated with CMYK. The challenge is that CMYK can’t reproduce every pantone color, so brand colors often need a dedicated spot ink.
That’s why a physical proof matters more than a digital mockup. A screen shows color in emitted light; film is printed in reflected light on a textured surface, and the ink sits on top of a metallic or matte base. A drawdown proof — an actual sample printed on your film — is the only way to really see how your colors will land. Digital mockups are useful for layout, but they’re not a color contract.
For photographic work on a pouch, wide-gamut digital printing and process color have limits. Fine screen detail and subtle gradients in a product photo can shift, so if your design leans on photography, plan to proof it on the actual film structure before the full run.
Finishing options
Matte, gloss, soft-touch, metallic, spot UV, and embossing all change how the package catches light and how the hand feels. Soft-touch gives a velvety premium feel that reads as luxury. Matte avoids glare under store fluorescent lighting and makes colors look richer. Gloss pops and looks bright. Metallic adds a shine behind the design. Spot UV adds gloss to specific areas against a matte base for a high-contrast effect. Each adds cost and complexity, so choose finishes that reinforce the brand’s position rather than applying them everywhere.

Designing for Shelf Impact (and Preventing Costly Mistakes)
Structural design: the pouch is a 3D object, not a flat file
The single most common design error is delivering artwork built for a flat rectangle. A pouch has a dieline — the flat template showing where folds, seals, gussets, and the zipper will sit. Everything must be positioned relative to that dieline. Bleed extends past the trim edge so no white line shows. Safe zones keep critical text away from the seal and fold lines where it would wrap or get trapped.
Panel layout that survives the real shelf
The front panel is what shoppers see first, but you also need to plan the back panel, the sides, and the base. The bottom gusset often gets a “bottom print” — brand name and flavor — for when the pouch is stacked. The seam needs to be accounted for too; a graphic can wrap around the seal edge and get lost. Work with the dieline as the source of truth and place each element in its physical home.
Typography and photos that read at glance distance
A shopper reads your package from several feet away under imperfect lighting, often while moving. Type that’s high-contrast, large enough, and not competing with the background wins. Fine serifs, thin strokes, and busy backgrounds all drop out at distance. The flavor name and the product type are the two strings you most need to keep legible. Make the bag size readable too — consumers check how much they’re getting, and that text often gets lost in the design.
Common design pitfalls: text sitting too close to the seal so it folds out of view, gusset prints that get hidden when the bag is filled, and graphics that clash with the zipper track. All three are preventable if the artwork is built on the dieline and checked against a finished sample.
Sustainable Snack Packaging — What’s Real, What’s Greenwash
Recyclable and mono-material pouches
The biggest movement in flexible packaging right now is the mono-material pouch. Historically, pouches were built from multiple different polymers — PET, nylon, foil, and PE — which made them effectively unrecyclable because they couldn’t be separated. A mono-material structure, usually all-PE or all-PP, can theoretically be collected in a plastics recycling stream. The trade-off: losing the combination of foil and PET reduces barrier performance, so mono-material pouches struggle with products that have long shelf-life, high-fat, or high-oxygen sensitivity.
Post-consumer recycled (PCR) content
Recycled content can be worked into a film, but food contact is the catch. FDA and comparable regulatory bodies have rules about what materials can touch food, and recycled content often can’t be used in the innermost, food-contact layer. That’s why you’ll commonly see PCR in a middle or outer layer, with virgin food-grade material still handling the food-contact surface. It’s a legitimate way to cut virgin plastic use, but the claim needs to be specific about where the recycled content sits.
Compostable options — the honest caveats
Compostable films exist and they work, but “compostable” is not the same as “it disappears in a home compost pile.” Industrial compostable materials require specific temperature, moisture, and time conditions that only commercial composting facilities provide. And those facilities are not evenly available. A pouch can be certified compostable and still end up in a landfill if your consumer has no access to commercial composting. Ask your supplier for the exact certification standard and check whether the infrastructure in your key markets can actually process it.
Source reduction and light-weighting
For many snack brands, the most credible sustainability lever is simply using less material while keeping the barrier. Thinner films, better design, and smarter structures cut weight and material per unit with no change to the consumer experience. This is source reduction — and it’s measurable and real, unlike some recycled-content claims. It also saves money on material and freight, which makes it a sustainability step and a cost step at the same time.
| Sustainability Option | Barrier Trade-off | Compliance Caveat | Best-Fit Snack Category |
|---|---|---|---|
| Mono-material recyclable | Lower barrier than multi-layer | Needs local recycling streams | Dry, short shelf-life items |
| PCR content | Moderate, depends on placement | Recycled content can’t touch food | Multi-serve, moderate barrier |
| Compostable | Lowest barrier, shortest shelf life | Needs industrial composting | Fresh, quick-turn items |
| Light-weighting | None if spec is right | Safest and most credible | Broad applicability |
Recycling infrastructure for flexible packaging is expanding, and collection programs have grown as mono-material formats become more common. But the practical reality varies sharply by region and by municipality. Treat “recyclable” as a claim that requires proof of a real collection path, not just a claim on the pack.
Compliance for Food Contact — What to Verify Before You Order
Why food-contact regulations are non-negotiable
Food-contact packaging is regulated because ink, adhesive, and film components can migrate into the food. Regulatory frameworks look at migration limits, heavy metals, and additives in inks and adhesives. In the United States, food-contact materials fall under FDA food-contact regulations. In the European Union, food-contact material regulations set migration limits and good manufacturing practice requirements. Different markets have different rules, which matters if you sell across regions.
What to ask a supplier for
A responsible supplier will hand you real documentation without being pushed. That includes a declaration of compliance for the finished pouch, migration test reports on the film structure, and confirmation that the inks and adhesives used are compliant for food contact. Food-grade certifications like ISO 22000 and ISO 9001 give you confidence in the manufacturing system behind the material. A supplier with FDA-compliant materials and a certified food-safety management system makes the compliance conversation much simpler.
Store brand and private-label considerations
If you’re supplying a retailer’s private label, you’ll inherit their artwork rules, often including standardized allergen and nutrition panels. Allergen claims need to be accurate and legally reviewed. Nutrition labeling placement is usually dictated by regulation, with required panels in specific positions. Have the artwork legally reviewed before printing, not after the run is done.
How to Choose a Snack Packaging Supplier (and What the Order Process Looks Like)
What MOQ really means (and how to read it)
Minimum order quantity sounds like a simple number, but it’s really a function of format, print method, material, and run length. A digital print run can be viable at much lower quantities than a rotogravure run, because there’s no cylinder to amortize. A mono-material structure with a zipper will have a different MOQ than a simple pillow bag.
Read MOQ in context. Don’t ask “what’s your minimum?” — ask what the minimum is for your specific pouch type, material, and print method. A supplier that understands your product category (like YLTPACK, a supplier established in 2005 specializing in customizable snack packaging solutions) can recommend a structure that fits your volume.
| Decision Factor | What to Ask | Why It Matters |
|---|---|---|
| Print method capability | Can you do digital, flexo, and gravure? | Determines flexibility across run sizes |
| Run length fit | What’s the realistic range for my spec? | Protects your cash flow early on |
| Lead time | How long from artwork to delivery? | Affects launch and replenishment planning |
| Quality control | What inspections happen before shipment? | Prevents defective batches reaching shelves |
| Certifications | Do you hold ISO 22000 / FDA compliance? | Verifies food-contact and system quality |
Typical lead times and the sampling path
Here’s the sequence a careful buyer walks through. First, the artwork and dieline are approved — this takes around 5 to 10 days depending on how many revisions are needed. Next, a sample or proof is produced so you can see and touch the actual pouch, which can take 3 to 7 days. Once you sign off, the production run happens, typically spanning 15 to 25 days depending on volume and print method. Then comes quality control and delivery, adding roughly 3 to 10 days. Total, a first order often runs 4 to 6 weeks from start to delivery.
A reputable supplier offers free samples so you can test structure, feel, and print quality before committing to a run. YLTPACK, for instance, provides free samples and works with clients to produce custom snack packaging tailored to their specific requirements.
Questions a careful buyer asks
The best questions come from experience. Ask about barrier specifications — can the supplier give you oxygen and moisture transmission rates for the proposed structure, or just a guess? Ask whether they hold film in stock, which shortens lead times. Ask about their proofing process and how they handle a color mismatch between a proof and the final run. Ask about their error-replacement policy in case of a defective batch. And ask whether they can scale the run as you grow, so you’re not locked into a supplier who can’t follow your volume curve.
Pros and Cons of Custom Pouches (The Honest Trade-offs)
Flexible snack packaging is the right answer for a lot of brands, but not all. Here’s the balanced picture.
| Pros | Cons |
|---|---|
| High brand flexibility across shapes and finishes | MOQ can be high for gravure-printed runs |
| Exceptional protection when barrier is specified correctly | Multi-layer structures can be hard to recycle |
| Strong shelf presence from large print panels | Pouch film can be prone to flex-cracking |
| Light weight lowers freight and material cost | Not ideal for products with very long shelf life |
| Fast design refresh cycles, especially with digital | Warehousing pouch stock requires clean, dry storage |
When a pouch is the right call
Choose a pouch when your product refreshes often, when you run multiple flavors or SKUs on one line, when you’re portioning snacks into single serves, or when shelf merchandising is central to the strategy. Granola, trail mix, chips, dried fruit, and all the single-serve snack categories live and breathe in pouches.
When it’s the wrong call (and what to use instead)
Skip the pouch for products that need a very long shelf life — think over a year with extreme oxygen or moisture sensitivity — where the barrier requirements push you toward structures that cost more and recycle worse. Same for products with extreme light sensitivity or those that need rigid protection from crushing. In those cases, a more rigid format wins despite the weight and cost. The honest answer is that no single format fits everything.
Common Mistakes and Best Practices (From Real Orders)
Mistakes that cost money
Skipping the physical proof is the most expensive shortcut in packaging. A digital mockup can’t reveal how your design lands on an actual film structure. Ignoring the dieline is the second — text wraps around the seal and becomes unreadable. Over-packaging is third, buying a high-barrier foil laminate for a product that only needs a simple moisture barrier. And ordering a huge first run before validating a new product is a mistake that ties up cash in unsold inventory.
Mistakes that hurt the brand
Color drift across reorders shows up when your brand color shifts batch to batch, which erodes trust in the brand itself. Artwork that’s unreadable at shelf distance means shoppers can’t tell what’s inside. And inconsistent quality between batches — some pouches glossy, some matte, some with a weak seal — makes the whole line look unreliable.
Best practices that pay off
Build a dieline-first workflow so artwork is always created against the real template. Lock a color standard with your supplier and re-verify it each reorder. Start with a moderate run and scale once the product proves itself. And keep a documented spec sheet for every SKU — film structure, dimensions, barrier values, print method, and finish — so every reorder is a reproduction of a known good, not a fresh guess.
FAQ — Snack Packaging Pouches
What’s the difference between a stand-up pouch and a flat-bottom pouch?
A stand-up pouch relies on a folded base gusset to stand, giving it a fuller, rounded profile. A flat-bottom pouch has a separately sealed flat base and four seal edges, which gives it a box-like, more premium posture and a larger print area. The flat-bottom uses more material and costs more per unit, but reads as a higher-end product on the shelf.
How do I know which film barrier my snack needs?
Work backward from how your product fails. Determine the oxygen, moisture, and light sensitivity of your snack, and decide your target shelf life. Then select a film structure that meets those transmission values rather than over-specifying. A supplier can help you test a sample against your actual conditions — and many, like YLTPACK, offer free samples for exactly this validation.
Can I get a custom pouch without a huge minimum order?
Yes, if you choose digital printing. Digital has no plate costs, so it works well for shorter runs and frequent design changes. Gravure printing requires cylinders that are only economical at high volumes. Your volume determines the right print method, which is why it’s worth discussing your actual order size with a supplier before committing.
How do I make sure my packaging meets food-safety rules?
Request documentation before you order. Ask for a declaration of compliance, migration test reports, and confirmation that inks and adhesives are food-contact compliant. A supplier with certifications like ISO 22000 and FDA-compliant materials makes this straightforward. Never accept “it should be fine” as an answer — get the paperwork.
How long does a custom pouch order usually take?
A typical first order runs about four to six weeks: roughly 5 to 10 days for artwork and dieline approval, 3 to 7 days for sampling, 15 to 25 days for production, and a few more days for QC and delivery. Reorders are faster because the spec and tooling are already established.
Are recyclable pouches actually recyclable in practice?
Only if your region has a collection stream that accepts them. Mono-material pouches are designed to be recyclable in theory, but local infrastructure determines whether they’re actually collected and processed. Always check what your target market can accept before making a recyclability claim on the pack.
Can I print the same design across different pouch sizes?
Yes, with preparation. The design needs to be adapted to each dieline because panel proportions, gusset placement, and seal positions change with size. The visual identity can stay consistent, but the artwork file must be re-laid-out per dieline so nothing gets cut off or wrapped.
Your Next Step — Getting Custom Snack Pouches Right
You now have the full picture. The path to a good result runs through a few clear decisions:
- Define your barrier need and target shelf life first.
- Build the artwork on the dieline, not flat.
- Choose the print method by your order volume.
- Demand compliance documentation before ordering.
- Treat sustainability as a real trade-off, then prototype before you scale.
The fastest way to turn this into a finished package is to talk to someone who works in this every day. If you’re ready to move from spec to sample, reach out to YLTPACK — a custom snack packaging manufacturer established in 2005, certified through ISO 22000 and FDA-compliant, offering free samples and packaging built exactly to your product’s needs. Share your snack category and target shelf life, and we’ll recommend a film structure, send a dieline for your artwork, or ship a sample pouch so you can see and feel the result before you commit to a run.
Get in touch at Feynman@yltpacking.com and let’s get your product on the shelf the way it deserves.