Flexible pouches have quietly taken over shelf space that cans, jars, and folding cartons held for decades. The reason is not aesthetics alone — it is freight economics, filling line throughput, and barrier performance that now rivals rigid formats at a fraction of the material weight.
For procurement teams and packaging engineers, the risk sits in the details. Choosing the wrong laminate structure or the wrong converting partner costs far more than the packaging itself: spoiled product, failed shelf-life validation, customs holds over missing compliance documents, and retooling delays that push a launch back by a full quarter.
This guide is a decision framework. It walks through material science, format selection, specification writing, regulatory documentation, supplier qualification, and cost optimization — in the sequence a sourcing team actually needs them.
Where Flexible Formats Have Taken Hold
Adoption is uneven across categories, and the pattern tells you something useful about which structures are proven and which are still maturing.
| Food Category | Dominant Pouch Format | Typical Structure | Shelf Life Range |
|---|---|---|---|
| Snacks & chips | Center-seal pillow, quad seal | BOPP/VMBOPP/CPP | 6–12 months |
| Roasted coffee | Flat bottom, stand-up with valve | PET/AL/PE or PET/VMPET/PE | 12–24 months |
| Pet food & treats | Flat bottom, stand-up with zipper | PET/NY/PE or PET/VMPET/PE | 12–18 months |
| Sauces & purees | Spouted pouch, retort pouch | PET/AL/NY/RCPP | 12–24 months |
| Powders & supplements | Stand-up, three-side seal | PET/AL/PE or PET/AlOx/PE | 18–36 months |
| Frozen & proteins | Vacuum pouch, gusseted bag | NY/PE or PET/NY/PE | 6–24 months (frozen) |
| Ready meals | Retort pouch | PET/AL/NY/RCPP | 12–36 months ambient |
Chapter 1: Understanding the Pouch Category
1.1 What Actually Defines a Laminated Pouch
A food packaging pouch is built from two or more film webs bonded together by adhesive lamination or extrusion lamination, then converted into a sealed three-dimensional container. That multi-web construction is what separates it from a single-web polyethylene bag.
Each web contributes a property no single film delivers on its own. This is why a spec sheet reads like PET12/AL7/NY15/RCPP70 rather than naming one plastic.

1.2 Pouch Anatomy: Four Functional Layers
Outer Print Layer
Usually PET (12µm), BOPP (18–20µm), or paper. It carries reverse-printed graphics protected between layers, delivers gloss or matte finish, and resists scuffing through distribution.
Barrier Layer
Aluminum foil, metallized PET (VMPET), EVOH, or transparent oxide coatings (AlOx/SiOx). This layer governs oxygen and moisture ingress — the single biggest determinant of shelf life.
Structural Layer
Biaxially oriented nylon (BOPA) adds puncture resistance and flex-crack durability. It becomes non-negotiable for bone-in proteins, frozen product handled at low temperature, and retort processing.
Food Contact Sealant Layer
LLDPE, CPP, or retort-grade CPP (RCPP). This layer sets seal strength, seal initiation temperature, and whether the pouch survives hot-fill or sterilization. It is also the layer that must satisfy food contact regulations.
1.3 Why Buyers Migrate Away from Rigid Packaging
The comparison below uses a 500g product as reference. Freight cube and warehouse footprint are where the numbers become hard to ignore.
| Metric | Stand-Up Pouch | Glass Jar | Metal Can | Folding Carton |
|---|---|---|---|---|
| Empty package weight | 8–15 g | 200–350 g | 50–90 g | 25–45 g |
| Package-to-product weight ratio | ~2–3% | ~45–70% | ~12–18% | ~6–9% |
| Empty units per standard pallet | Very high (flat-shipped) | Low | Moderate | High (flat blanks) |
| Inbound storage volume index | 1.0 | 12–18 | 8–14 | 2–3 |
| Typical ambient shelf life | 6–36 months | 12–36 months | 24–60 months | 3–12 months |
| Breakage risk in transit | Very low | High | Low (denting) | Moderate (crushing) |
| Shelf-facing print area | High | Label-limited | Label-limited | High |
Chapter 2: Format Selection — Matching Structure to Product
2.1 Stand-Up Pouch (Doypack)
The default for retail flexible packaging. K-seal bottoms give better standing stability at higher fill weights; round-bottom versions look cleaner on shelf but tip more easily when underfilled. Works best between roughly 50g and 1.5kg.

2.2 Flat Bottom / Box Pouch
Eight-side seal construction with five printable panels. Superior stability at 500g–5kg fill weights and a distinctly premium shelf presence. It has become the standard for specialty coffee and higher-tier pet food.
2.3 Three-Side Seal and Sachets
The lowest-cost option for single-serve, condiment, sample, and trial-size applications. Highly compatible with high-speed form-fill-seal equipment, and the format of choice for stick packs and drink powders.
2.4 Center-Seal Pillow and Quad Seal
Most efficient film usage per unit of product, which is why chips, cereal, and high-volume snacks stay with it. Quad seal adds side gussets for better stacking and a printable side panel.
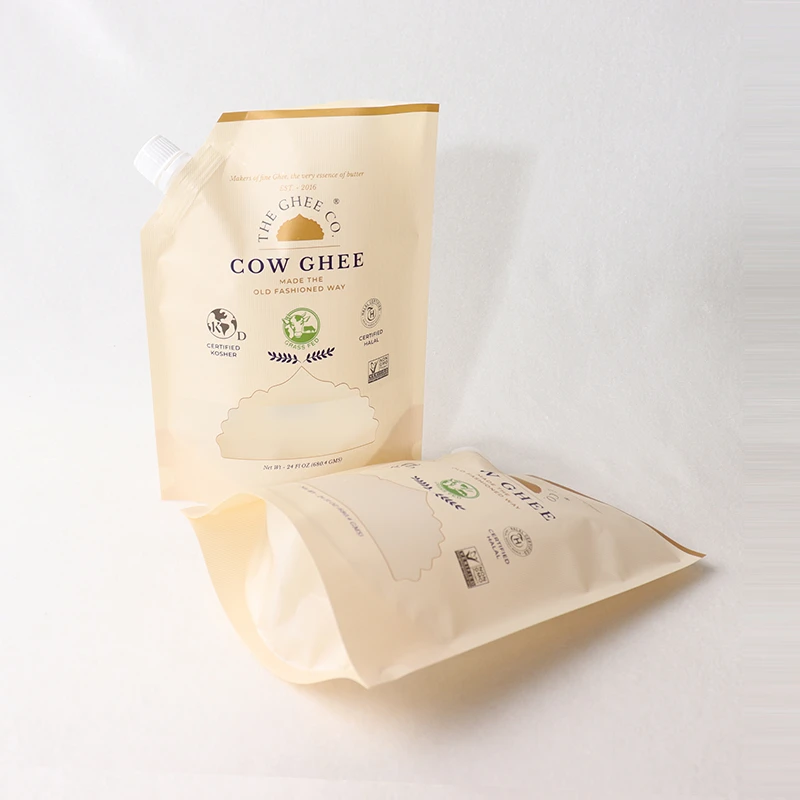
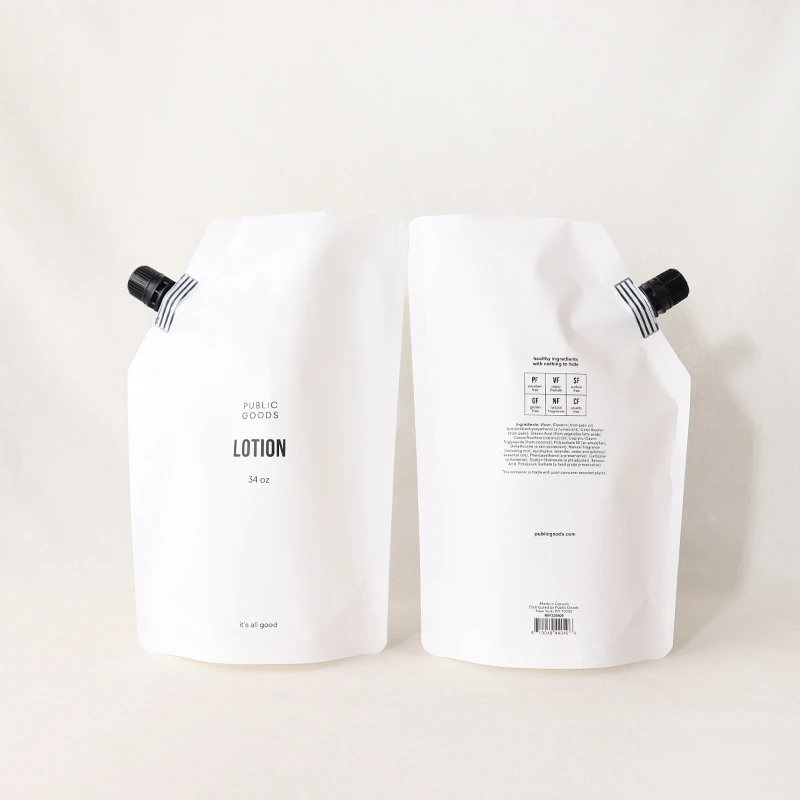
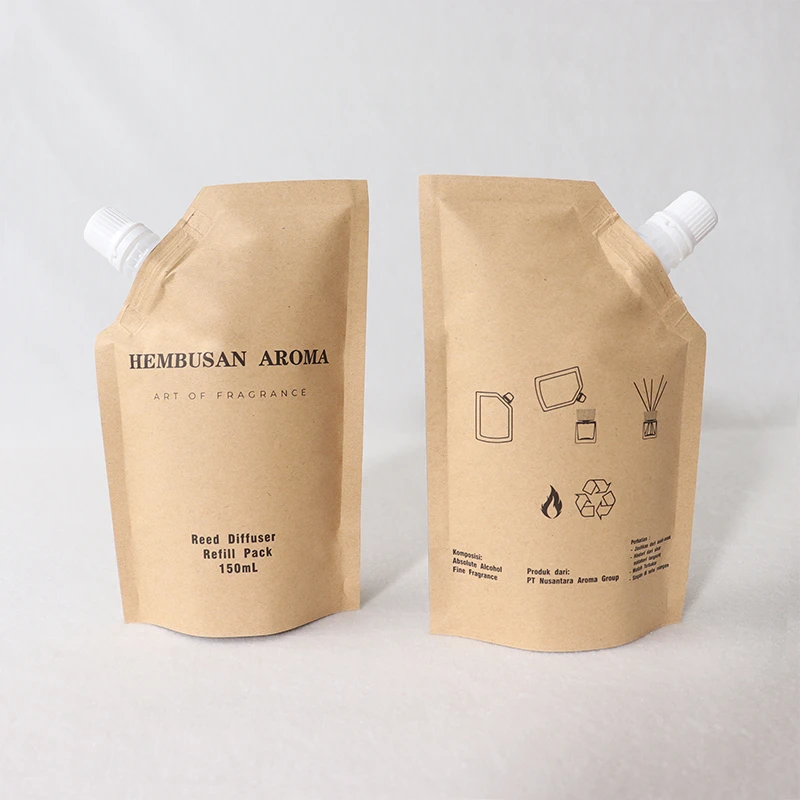
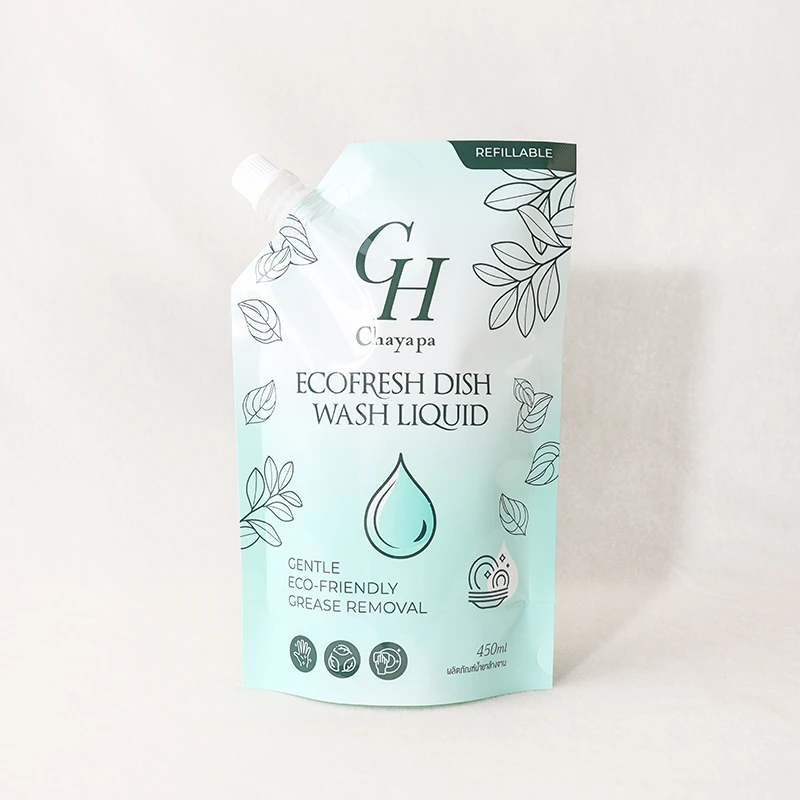
2.5 Spouted Pouch
Fitment diameter drives application: 6.3mm for baby food and thin purees, 8.6mm for sauces and thicker liquids, 9.6mm and above for beverages and viscous products. Child-resistant and tamper-evident cap options are available, along with hot-fill and aseptic-compatible structures.
2.6 Retort Pouch
Built to survive sterilization at 121°C and above, with holding times up to 40 minutes. Requires RCPP sealant and, for most ambient shelf-stable applications, a foil-based laminate. Ready meals, wet pet food, and shelf-stable soups depend on it.
2.7 Vacuum and Skin Pack Pouches
Nylon-based, high-puncture-resistance structures for fresh proteins, cheese, and sous-vide. Seal integrity matters more here than in any other format, because vacuum loss is immediately visible to the consumer.
| Format | Recommended Fill Range | Typical Shelf Life | Filling Equipment | Tooling Required | Unit Cost Index |
|---|---|---|---|---|---|
| Stand-up pouch | 50 g – 1.5 kg | 6–24 months | Rotary premade filler | Bottom die | 1.0 |
| Flat bottom pouch | 250 g – 5 kg | 12–24 months | Rotary premade filler | Specialized die set | 1.3–1.5 |
| Three-side seal | 2 g – 200 g | 6–24 months | HFFS / premade | Minimal | 0.5–0.7 |
| Center-seal pillow | 20 g – 1 kg | 6–12 months | VFFS roll stock | Forming collar | 0.4–0.6 |
| Quad seal | 100 g – 2 kg | 6–18 months | VFFS with gusset unit | Forming set | 0.7–0.9 |
| Spouted pouch | 50 ml – 3 L | 9–24 months | Spout filler / aseptic | Die + fitment tooling | 1.6–2.2 |
| Retort pouch | 80 g – 2 kg | 12–36 months | Retort-compatible filler | Die + retort validation | 1.8–2.4 |
| Vacuum pouch | 100 g – 5 kg | Varies by chain | Chamber / thermoform | Minimal | 0.8–1.1 |
Chapter 3: Barrier Engineering — The Spec That Sets Shelf Life
3.1 Reading OTR and WVTR
Oxygen Transmission Rate (OTR) is measured in cc/m²/day at defined temperature and humidity, per ASTM F1927 or ASTM D3985. Water Vapor Transmission Rate (WVTR) is measured in g/m²/day per ASTM F1249.
Lower is better, but there is a point of diminishing return. A powder with an 18-month target does not need foil-level barrier if the product is dry, low-fat, and shipped in stable conditions. Over-specification is one of the most common — and most expensive — sourcing mistakes.
3.2 Barrier Performance by Structure
| Structure | Total Thickness | OTR (cc/m²/day) | WVTR (g/m²/day) | Light Barrier | Microwave Safe | Recycling Stream | Typical Use |
|---|---|---|---|---|---|---|---|
| PET/PE | 70–100 µm | 50–110 | 5–10 | None | Yes | Mixed / limited | Short shelf life, dry goods |
| PET/VMPET/PE | 85–120 µm | 0.5–1.5 | 0.3–0.8 | High | No | Mixed | Snacks, coffee, treats |
| PET/AL/PE | 95–130 µm | <0.1 | <0.1 | Total | No | Not recyclable | Powders, supplements |
| PET/AL/NY/RCPP | 130–180 µm | <0.05 | <0.05 | Total | No | Not recyclable | Retort meals, wet pet food |
| PET/EVOH/PE | 90–130 µm | 0.5–2.0 | 3–7 | None | Yes | Mixed | Oxygen-sensitive, transparent |
| PET/AlOx/PE | 80–110 µm | 0.5–1.5 | 0.5–1.5 | None | Yes | Mixed | Premium transparent, retort-capable |
| Kraft/VMPET/PE | 120–160 µm | 0.8–2.0 | 0.5–1.2 | High | No | Mixed | Natural-positioning brands |
| PE/PE mono-material | 100–140 µm | 1.5–8 (coated) | 1.5–4 | Optional | Yes | PE store drop-off | Recyclable dry goods |
| BOPP/BOPP mono-material | 90–130 µm | 1.0–5 (metallized) | 0.3–1.0 | Optional | Yes | PP stream | Snacks, confectionery |
Values are typical laboratory ranges at 23°C and 50% RH. Always request converter-specific test data for your exact structure.
3.3 Matching Barrier to Product Sensitivity
- Oxygen-sensitive (coffee, nuts, oils, cured meat): target OTR below 1 cc/m²/day; below 0.1 for multi-year ambient shelf life.
- Moisture-sensitive (crisps, freeze-dried, effervescent powders): WVTR below 0.5 g/m²/day, with attention to seal integrity at the closure.
- Light-sensitive (dairy powder, vitamins, omega oils): metallized or foil layer, or high-opacity white/black pigmented sealant.
- Aroma retention (spices, tea, coffee): barrier plus low-scalping sealant; PE scalps flavor compounds more than CPP.
Foil is genuinely required when you need near-zero transmission, total light block, and a proven ambient retort structure. If none of those apply, metallized or oxide-coated films usually deliver adequate protection at lower weight and better formability.

3.4 Shelf-Life Modeling and Validation
Accelerated aging at 38°C/90% RH is a common protocol for moisture-driven failure; oxidation-driven products are typically studied at 35–40°C with periodic sensory and peroxide value testing. Real-time confirmation should run in parallel.
For roasted coffee, a one-way degassing valve is mandatory — CO₂ release peaks in the first 48–72 hours after roasting and will otherwise distort or burst the pouch. Target residual headspace oxygen is generally under 2% for whole bean and under 1% for ground coffee.
Request barrier test reports and seal strength data before committing to cylinder engraving. Reworking a spec after tooling is where projects lose weeks.
Chapter 4: Sustainable Options Without Sacrificing Barrier
4.1 Mono-Material Recyclable Structures
All-PE laminates built on machine-direction-oriented PE (MDO-PE) now approach the stiffness and printability of PET/PE while remaining compatible with polyethylene store drop-off collection. All-PP structures serve snack and confectionery categories well.
The realistic barrier ceiling for coated mono-material sits around 1 cc/m²/day OTR — strong enough for a large share of dry goods, not yet a substitute for foil in retort or multi-year ambient applications.
4.2 Paper-Based and Hybrid Pouches
Fiber-based pouches typically need 80–90% fiber content by weight to qualify for paper recycling streams in most regions. The constraint is moisture: paper laminates need a functional barrier coating, and they run slower on vertical form-fill-seal lines because of stiffness and dead-fold behavior.
4.3 Compostable and Bio-Based Films
PLA, PBAT, and cellulose-based films certified to EN 13432, BPI, or TÜV OK Compost serve brands with a clear composting narrative. Be candid about trade-offs: shorter shelf life, narrower heat-seal windows, sensitivity to warehouse heat, and limited industrial composting infrastructure in many markets.
4.4 Downgauging
Often the highest-return sustainability lever. Replacing a 12µm PET/12µm PET structure with a single oriented layer, or moving from 80µm to 65µm sealant where seal strength allows, can cut material use 10–20% with no barrier loss and no recycling-stream change.
4.5 Regulation Reshaping Specifications
The EU Packaging and Packaging Waste Regulation sets recyclability requirements that take effect through the late 2020s, with design-for-recycling criteria that penalize multi-material laminates. Extended Producer Responsibility fee structures in the EU and a growing number of North American states are eco-modulated — non-recyclable structures carry higher fees.
PFAS restrictions on food-contact materials now apply in multiple U.S. states and across the EU. Exporters should hold current PFAS-free declarations for every structure in their portfolio.
| Sustainable Option | Barrier Capability | Certification | Line Speed Impact | Best Fit | Key Limitation |
|---|---|---|---|---|---|
| Mono-material PE | Medium–High | How2Recycle, RecyClass | 5–15% slower | Dry goods, pet treats, frozen | Lower heat resistance |
| Mono-material PP | Medium–High | RecyClass | Minimal | Snacks, confectionery | Limited collection in some regions |
| Paper hybrid | Low–Medium | FSC, fiber stream | 10–25% slower | Tea, dry mixes, natural brands | Moisture and grease sensitivity |
| Compostable film | Low | EN 13432, BPI, OK Compost | 15–30% slower | Short-cycle, food service | Shelf life and infrastructure |
| Downgauged conventional | Unchanged | N/A | None | Any existing SKU | Requires seal validation |
Chapter 5: Writing a Custom Specification That Prevents Errors
5.1 Dimensional Specification
State width, height, bottom gusset depth, and side gusset separately, and clarify whether measurements are flat (unfilled) or finished (filled). This single ambiguity causes more rejected first runs than any other spec error — a filler expecting 130mm finished width will not run a pouch drawn to 130mm flat.
Fill volume should be validated with bulk density, not assumed. A 200g whole bean coffee and a 200g protein powder need very different pouch geometry.
5.2 Print and Artwork Requirements
Rotogravure delivers the finest detail and lowest cost per unit at high volume, but requires engraved cylinders per color. Flexography suits medium runs with lower plate investment. Digital printing eliminates tooling entirely and is the practical choice for launches, regional SKUs, and variable-data projects.
Provide vector artwork (AI, PDF, or EPS) with fonts outlined, raster elements at 300 dpi or higher at final size, CMYK color mode with spot colors defined, and 3–5mm bleed. Keep critical text at least 5mm from seal areas.
Color Management
Pantone references should be specified with the substrate noted, since dot gain on film differs substantially from paper. For any color-critical brand, request a printed press proof on the actual laminate rather than approving a digital proof — screen-to-film color shift is real and expensive to discover after 50,000 pouches.
5.3 Finishing and Convenience Features
- Opening: tear notch, laser scoring for straight-line tear, easy-open perforation
- Reclosure: standard zipper, pocket zipper, slider, press-to-close, child-resistant closure
- Functional: one-way degassing valve, hang hole, euro slot, handle punch, vent hole for microwave steam
- Finish: matte or gloss lamination, spot gloss varnish, soft-touch coating, registered matte, cold foil or holographic accents
5.4 Barcode, Coding, and Traceability
Barcodes should be printed with sufficient quiet zone and verified for scannability — grade C or better under ISO/IEC 15416. Reserve a coding window with a matte or uncoated surface where inkjet or laser date coding will be applied; coding onto high-gloss varnish smears.
| Spec Field | What to Provide | Common Mistake | Impact If Wrong |
|---|---|---|---|
| Dimensions | W × H × gusset, flat or finished stated | Mixing flat and finished | Pouch fails on filler |
| Structure | Layer-by-layer with gauge in µm | Naming only “high barrier” | Barrier mismatch, short shelf life |
| Sealant | Type and thickness, process temperature | Standard PE for hot-fill | Seal failure, leakage |
| Artwork | Vector, outlined fonts, dieline layer | Low-res raster logos | Blurred print, reprint cost |
| Color | Pantone codes plus press proof approval | Approving digital proof only | Off-brand color across run |
| Features | Zipper type, notch position, valve location | Omitting valve placement | Rework or re-tooling |
| Coding area | Location and surface finish | Coding over gloss varnish | Illegible date codes, retailer rejection |
| Packing | Units per carton, carton dimensions, pallet pattern | Leaving it to the supplier | Warehouse and freight inefficiency |
Chapter 6: Compliance, Testing, and Documentation for Cross-Border Shipments
6.1 Food Contact Regulations by Market
The United States governs food contact materials under FDA 21 CFR, with the relevant sections depending on polymer type — 177.1520 for olefin polymers, 177.1630 for PET, and 175.300 for resinous coatings among others.
The European Union applies Framework Regulation 1935/2004 together with Regulation 10/2011 for plastics, requiring overall and specific migration testing under defined food simulants and time-temperature conditions. China’s GB 4806 series covers plastics, adhesives, inks, and composite materials, and Japan operates a Positive List system for synthetic resins.
A structure approved in one market is not automatically compliant in another. Adhesives and inks are frequently the point of divergence.
6.2 Documentation Buyers Should Require
- Declaration of Compliance for the finished laminate, not just individual films
- Overall and specific migration test reports against the correct food simulant
- Heavy metal content statement (typically referencing the 100 ppm sum limit for lead, cadmium, mercury, hexavalent chromium)
- Allergen and BSE/TSE-free declarations
- PFAS-free statement covering all layers, inks, and coatings
- Material safety and shelf-life storage recommendations for the unfilled pouches
6.3 Facility-Level Certifications
These verify the production environment, not the individual product. Both matter.
- BRCGS Packaging Materials — hygiene zoning, foreign body control, traceability; widely required by European and UK retailers.
- ISO 22000 / FSSC 22000 — food safety management systems with hazard analysis applied to packaging manufacture.
- SGS or Intertek audit reports — third-party verification of facility conditions and process controls.
6.4 Performance Testing Protocols
| Test | Standard | What It Confirms | Typical Acceptance Threshold |
|---|---|---|---|
| Seal strength | ASTM F88 | Heat seal integrity | ≥ 25 N/15mm (standard), ≥ 40 N/15mm (retort) |
| Burst / internal pressure | ASTM F1140 | Seal resistance to pressure | ≥ 30 kPa held 30 seconds |
| Drop test | ASTM D5276 | Distribution survivability | No leakage after 1.2 m drops, multiple orientations |
| Puncture resistance | ASTM F1306 | Film durability under point load | Product-dependent; higher for bone-in and granular |
| Bond strength | ASTM F904 | Lamination adhesion | ≥ 2.0 N/15mm between layers |
| Barrier | ASTM F1927 / F1249 | OTR and WVTR | Per structure specification |
| Destination Market | Governing Regulation | Required Document | Typical Testing Lead Time |
|---|---|---|---|
| United States | FDA 21 CFR 174–178 | FDA compliance statement, PFAS declaration | 7–15 days |
| European Union | EC 1935/2004, EU 10/2011 | Declaration of Compliance + migration report | 15–25 days |
| United Kingdom | Retained EU law + BRCGS retailer demand | DoC + facility certificate | 15–25 days |
| Canada | Food and Drugs Act, Division 23 | Letter of No Objection or equivalent | 10–20 days |
| China | GB 4806 series | GB test report per layer and composite | 15–20 days |
| Japan | Positive List system | Positive List conformity statement | 15–25 days |
| Australia / NZ | FSANZ Standard 1.4.3 | Compliance declaration | 10–15 days |
Chapter 7: Evaluating Food Pouch Packaging Suppliers
7.1 Supplier Categories
Converters own printing, lamination, and pouch-making in-house. They control quality end to end, can adjust structures, and can produce test data on request. Trading intermediaries broker capacity — sometimes efficiently, but structure transparency and problem resolution suffer. Regional distributors hold stock pouches and serve fast, low-volume needs without customization depth.
For custom food pouch packaging with genuine barrier and compliance requirements, working directly with the converter removes a layer of translation from every technical conversation.
7.2 Capability Audit Questions
- Which printing methods are in-house, and what is the maximum color count and repeat length?
- Is lamination solventless, solvent-based, or both — and what residual solvent limit is applied?
- Is there a clean or controlled production area for food-contact converting?
- What testing equipment exists on site (OTR/WVTR, seal strength, bond strength, migration pre-screening)?
- What is the maximum web width and annual converting capacity?
- What curing time is applied after lamination before converting?
7.3 Order Quantity Structures
Minimum order quantities are driven primarily by print cylinder economics and film run efficiency. A gravure press needs a minimum web length to reach stable color registration, and that floor sets the MOQ regardless of what the buyer wants.
| Printing Method | Typical MOQ Band | Tooling Requirement | Best Suited To |
|---|---|---|---|
| Digital | 1,000 – 10,000 pouches | None | Launches, seasonal SKUs, variable data |
| Flexographic | 10,000 – 50,000 pouches | Photopolymer plates | Mid-volume, moderate color count |
| Rotogravure | 30,000 – 100,000+ pouches | Engraved cylinders per color | High volume, long-term SKUs |
| Roll stock (any method) | By linear meters / kg | Method-dependent | Form-fill-seal operations |
A useful negotiation tactic: commit to a single production run that satisfies the press minimum, then schedule staged releases from the supplier’s warehouse. This preserves cash flow and storage space without triggering repeat setup.
7.4 Lead Time Planning
| Stage | Typical Duration | Notes |
|---|---|---|
| Structure consultation and quotation | 1–3 days | Faster with complete product data |
| Physical samples (unprinted) | 5–10 days | For fit and line trial |
| Artwork and dieline confirmation | 3–7 days | Buyer-controlled; often the longest variable |
| Cylinder engraving | 7–12 days | Skipped for digital printing |
| Printing and lamination | 7–12 days | Includes color approval on press |
| Curing | 3–7 days | Non-negotiable for solvent-based lamination |
| Converting and QC | 5–8 days | Zipper, spout, and valve add time |
| Ocean transit | 20–40 days | Route and season dependent |
Budget 45–60 days ex-works for a first custom order and 25–35 days for repeats. Add a 10–14 day buffer for first-run projects where color approval may require a second press pass.
7.5 Quality Control and Incoming Inspection
Specify AQL sampling in the purchase agreement rather than leaving inspection standards undefined. A common framework is ISO 2859-1 General Inspection Level II with AQL 0.65 for critical defects, 2.5 for major, and 4.0 for minor.
Define the categories explicitly: seal leakage and food-contact contamination are critical; wrong dimensions, missing zipper function, and misregistered print are major; minor color variation within agreed tolerance and small cosmetic marks are minor.
7.6 Red Flags
- Reluctance to disclose the full layer structure with gauges
- No in-house or third-party test reports available on request
- Lead time quotes that omit lamination curing entirely
- No separation between food-grade and industrial production
- Samples that arrive without any structure documentation
- Pricing that changes materially after artwork is submitted
| Criterion | Weight | Evidence to Request | Pass Threshold |
|---|---|---|---|
| Food safety certification | 20% | ISO 22000 / BRCGS / FSSC certificate | Valid, in scope for pouches |
| Barrier test capability | 20% | OTR/WVTR reports for your structure | Data provided pre-order |
| Regulatory documentation | 15% | DoC, migration, PFAS statements | Complete for destination market |
| In-house converting | 15% | Facility list, equipment photos, audit | Printing + lamination + pouch making |
| Sample responsiveness | 10% | Physical samples with spec sheet | Delivered within 10 days |
| Technical communication | 10% | Written structure recommendation | Reasoned, not generic |
| Track record in category | 10% | References in comparable products | Verifiable examples |
Chapter 8: Cost Drivers and Order Optimization
8.1 What Actually Drives Pouch Cost
| Variable | Relative Impact | Optimization Lever |
|---|---|---|
| Film structure and barrier level | High | Specify to actual shelf-life need, not maximum |
| Total gauge / thickness | High | Downgauge with seal validation |
| Surface area (pouch size) | High | Optimize geometry to true fill volume |
| Run length | High | Consolidate SKUs into single runs |
| Color count | Medium | Design within 6–8 colors; use substrate as a color |
| Format complexity | Medium | Stand-up instead of flat bottom where shelf allows |
| Add-on features | Medium | Audit whether zipper or valve is truly used |
| Tooling | One-time | Amortize across SKU family or use digital |
8.2 Consolidation Strategies
Design SKU families that share a common base structure and pouch size, varying only the print. Where flavor or variant counts are high, a generic base print with digital overprint for variable panels can cut tooling investment dramatically.
Standardizing on two or three structures across an entire product line also simplifies compliance documentation and shortens repeat lead times.
8.3 Tooling Amortization Logic
Gravure cylinder investment is one-time and reusable across repeat orders. The break-even against digital printing generally falls somewhere between 30,000 and 60,000 pouches per design, depending on color count and pouch size.
Below that, digital printing is usually the better economic decision and carries far less risk if artwork changes. Above it, gravure wins decisively on per-unit cost and print quality consistency.
8.4 Total Cost Beyond the Pouch
The pouch itself is rarely the largest line item in a packaging decision. Filling line throughput, product giveaway from oversized headspace, freight cube, damage rates in distribution, and returns from seal failure all move the total number more than a fractional difference in unit cost.
A pouch that runs 15% slower on the filler will erase any savings from a cheaper structure within a single production shift.
Chapter 9: Filling Line Compatibility
9.1 Pre-Made Pouch vs. Roll Stock
Pre-made pouches suit rotary pouch fillers, offer superior print registration and finishing quality, and support complex formats like flat bottom and spouted. Roll stock feeds vertical or horizontal form-fill-seal machines at higher speeds and lower cost per unit, but limits format and finishing options.
The decision usually follows volume: below roughly 5 million units annually, pre-made pouches often deliver better total economics once changeover and waste are counted.
9.2 Runnability Factors
- Coefficient of friction: typically 0.20–0.35 for smooth machine feeding; too low causes slipping, too high causes drag
- Film stiffness: critical for pouch opening on rotary fillers and forming on VFFS collars
- Static control: anti-static treatment prevents pouch nesting and powder cling
- Seal window: a wider temperature window tolerates line speed variation; specify the range, not a single number
- Registration marks: confirm eye mark size, color, and position with the machine manufacturer’s spec
9.3 Pilot Run Protocol
Request 500–2,000 unprinted or plain-printed pouches for a line trial before full production. Measure fill accuracy, seal strength across the full width, reject rate, machine speed against baseline, and pouch standing stability at target fill weight.
Document results in writing and share them with the converter. Adjustments to gauge, COF, or seal layer are inexpensive at this stage and costly later.
Chapter 10: Implementation Roadmap
| Phase | Key Activities | Deliverable | Typical Duration | Owner |
|---|---|---|---|---|
| 1. Product assessment | Define sensitivity, shelf life, fill weight, market | Technical brief | 3–5 days | Buyer |
| 2. Structure selection | Barrier modeling, format matching | Recommended structure with test data | 3–7 days | Converter |
| 3. Sample validation | Physical samples, seal and fit checks | Approved sample set | 7–14 days | Joint |
| 4. Artwork and dieline | Dieline issue, artwork prep, proofing | Signed-off press-ready file | 7–14 days | Buyer |
| 5. Compliance package | DoC, migration, certificates | Complete document file | 10–25 days | Converter |
| 6. Pilot run | Line trial, measurement, adjustment | Trial report | 5–10 days | Joint |
| 7. Production | Printing, lamination, curing, converting, QC | Finished goods + inspection report | 20–30 days | Converter |
| 8. Delivery | Shipping, customs, incoming inspection | Accepted stock | 20–40 days ocean | Joint |
10.2 Common Project Failure Points
- Artwork revisions requested after cylinder engraving — the cost and delay are both fully avoidable
- Skipping shelf-life validation to hit a launch date, then discovering rancidity in month four
- Under-specifying barrier to reduce unit cost, then absorbing product write-offs that dwarf the savings
- Ignoring lamination curing time when building the production schedule
- Underestimating ocean freight variability during peak season
Frequently Asked Questions
What barrier structure does my product actually need?
Start with the failure mechanism. Oxidation-driven products such as coffee, nuts, and oils need OTR below 1 cc/m²/day, and below 0.1 for multi-year ambient shelf life — pointing toward foil or high-performance metallized structures. Moisture-driven products such as crisps and freeze-dried items need WVTR below 0.5 g/m²/day. Dry, stable goods with a 6–12 month target are usually well served by PET/VMPET/PE or a coated mono-material.
What is a typical minimum order quantity for custom printed pouches?
It depends almost entirely on printing method. Digital printing starts around 1,000–10,000 pouches with no tooling. Flexographic typically begins at 10,000–50,000, and rotogravure at 30,000 or more per design because of cylinder economics. For new launches or test markets, digital printing lets you validate demand before committing to engraved tooling.
How long does a first custom pouch order take from artwork to delivery?
Plan on 45–60 days ex-works: roughly one to two weeks for artwork and dieline sign-off, one to two weeks for cylinder engraving, two weeks for printing and lamination including curing, and one week for converting and quality control. Add ocean transit of 20–40 days depending on destination. Repeat orders using existing tooling typically run 25–35 days ex-works.
Can recyclable mono-material pouches match foil barrier performance?
Not yet, and any supplier claiming otherwise is overselling. Coated mono-material PE and PP structures currently reach around 1 cc/m²/day OTR and 1.5 g/m²/day WVTR — sufficient for a large share of dry goods, snacks, pet treats, and 6–12 month shelf-life products. For retort processing, multi-year ambient shelf life, or highly oxygen-sensitive oils, foil or high-barrier metallized laminates remain necessary.
Which certifications should a food pouch supplier hold?
ISO 22000 or FSSC 22000 for food safety management should be considered baseline. FDA 21 CFR compliance documentation is essential for the U.S. market, and a Declaration of Compliance with migration testing for the EU. BRCGS Packaging Materials matters most for European and UK retail supply. Beyond certificates, ask whether the supplier can produce structure-specific test reports on request — that capability is often more revealing than the certificates themselves.
Are pouches suitable for retort, hot-fill, and microwave applications?
Yes, with the right sealant. Retort at 121°C and above requires RCPP sealant with a nylon structural layer, usually paired with foil for ambient shelf stability. Hot-fill at 85–95°C runs on CPP-based structures. Microwaveable pouches require a metal-free laminate — PET/AlOx/PE or PET/EVOH/PE — plus a steam vent or self-venting seal. Each thermal process needs its own validation before production release.
How is shelf life validated before committing to a full production run?
Use accelerated aging at elevated temperature and humidity, commonly 38°C and 90% RH for moisture-sensitive products, alongside real-time storage. Measure headspace oxygen at intervals, track peroxide value or sensory attributes for fat-containing products, and verify seal integrity throughout. Request barrier and seal strength reports from the converter before tooling is committed, and run the validation on samples made with the exact production structure.
What file formats and artwork specifications are required for printing?
Supply vector files in AI, PDF, or EPS format with all fonts converted to outlines. Raster elements should be 300 dpi or higher at final print size. Use CMYK color mode with spot colors named as Pantone references, include 3–5mm bleed, keep critical text 5mm clear of seal areas, and place the dieline on a separate labeled layer as a spot color set to overprint.
How should incoming pouch shipments be inspected?
Apply an agreed AQL sampling plan — ISO 2859-1 Level II with AQL 0.65 for critical, 2.5 for major, and 4.0 for minor defects is a workable default. Verify finished dimensions against specification, spot-check seal integrity with a water immersion or vacuum leak test, confirm print color against the approved press proof, and scan barcodes on a sample from multiple cartons.
Can existing filling equipment run a new pouch structure without modification?
Often yes, but never assume it. Coefficient of friction, film stiffness, static behavior, and seal window all shift when a structure changes — even at identical dimensions. Request 500–2,000 trial pouches, run them at production speed, and document reject rate, seal strength, and throughput before releasing a full order.
Conclusion: Specification Discipline Beats Price Shopping
The decision sequence is consistent across every successful pouch project: define product sensitivity, select the barrier structure that meets it without over-engineering, choose the format that fits fill weight and shelf presentation, add only the features that earn their place, secure compliance documentation for the destination market, qualify the supplier against evidence rather than claims, and validate with a pilot run.
Teams that invest in that sequence upfront eliminate the overwhelming majority of downstream packaging failures. Teamsthat skip it usually pay for the lesson in write-offs, delayed launches, and emergency reorders.
Work With a Technical Partner, Not Just a Vendor
YLTPACK has manufactured custom flexible packaging since 2005, producing food pouch packaging for brands across snacks, coffee, pet nutrition, supplements, sauces, and frozen categories. Production is certified to ISO 22000 and supported by FDA-compliant material documentation, with migration and barrier test reports available for every structure we supply.
Every order is engineered around your specification — structure, dimensions, barrier target, closure system, and finishing. Free physical samples are available so your team can validate fit, seal performance, and line runnability before any tooling commitment is made.
To receive a tailored structure recommendation and sample set, send us the following:
- Product type, bulk density, and fat or moisture content
- Target shelf life and storage conditions
- Fill weight or volume per unit
- Destination market or markets
- Estimated annual volume and preferred format
- Filling equipment type, if already installed
Our engineering team will respond with a recommended laminate structure, expected OTR and WVTR values, format options, and a documented compliance path for your destination market — reviewed as a technical consultation, not a sales pitch.
Contact: Feynman@yltpacking.com